Professional NdFeB Magnets Manufacturer and Sales Center
High Quality
High Performance
Technology Support
China’s position in the permanent-magnet supply chain makes it a vital starting point for evaluating Dy Doped Neodymium Magnets manufacturers. The U.S. Geological Survey reported approximately 270,000 metric tons of rare-earth mine production in China during 2024. The International Energy Agency also identifies China as the dominant country in rare-earth refining and permanent-magnet manufacturing. These figures explain the country’s strong manufacturing base, but they do not automatically prove quality.
Dysprosium improves coercivity and helps neodymium magnets retain performance at elevated temperatures. This matters in electric-vehicle motors, industrial robots, wind turbines, and compact aerospace systems. Experienced buyers should examine grain-boundary diffusion methods, dysprosium distribution, magnetic test records, coating durability, and batch traceability. A polished catalog is not enough. Neither is a low price.
Rare-earth industry expert Dudley Kingsnorth has often stated, “Rare earths are not rare; they are just difficult to extract.” His observation also reflects the magnet market. Material availability, processing consistency, and environmental controls influence the final product. Leading Chinese manufacturers should therefore be judged through verifiable evidence, including ISO certifications, third-party testing, production capacity, and field experience.
Some comparisons remain imperfect. Public reports may combine different rare-earth categories, while manufacturers may present magnetic data under different testing conditions. This article examines China’s leading suppliers with that limitation in mind. It focuses on technical capability, reliability, customization, and practical application performance rather than promotional rankings alone.
Dy-doped neodymium magnets are neodymium-iron-boron magnets containing a controlled addition of dysprosium. The doping process changes the grain boundaries and improves resistance to heat. This matters in motors, sensors, pumps, and compact generators operating above ordinary room temperature.
Their key property is higher coercivity, which helps prevent irreversible demagnetization. A well-made magnet can retain useful magnetic strength near 150°C, although the exact limit depends on grade, geometry, coating, and working conditions. Dysprosium also supports stable performance when strong magnetic fields reverse repeatedly. The trade-off is important. Excessive dysprosium can reduce remanence and raise material costs. More is not always better.
From a manufacturing perspective, uniform distribution is critical. Engineers inspect composition, density, magnetic orientation, surface finish, and temperature performance. A small chip on a sharp edge may expose the material to corrosion, even when the coating looks intact. Nickel-based coatings are common, while other protective systems suit special environments. Test data should match the customer’s actual duty cycle, not only room-temperature measurements. This is where specifications can become misleading. A magnet may pass a laboratory test yet lose performance after months of vibration and heat. Careful suppliers provide batch records, dimensional checks, and thermal test results. Field feedback still deserves attention. No formula replaces it.
China’s role in dysprosium-doped neodymium magnet manufacturing is unusually strong. The U.S. Geological Survey estimated China produced 240,000 metric tons of rare-earth oxides in 2023. That represented roughly two-thirds of global mine output. The International Energy Agency reported that China controlled about 90% of rare-earth refining and 94% of permanent-magnet production in 2023. These figures explain why Chinese manufacturers remain central to high-performance magnet supply.
Dysprosium improves coercivity, helping NdFeB magnets resist demagnetization at elevated temperatures. This matters in electric motors, industrial equipment, and compact generators. Modern Chinese factories increasingly use grain-boundary diffusion to place dysprosium near the magnet surface. The method can reduce heavy rare-earth consumption while preserving thermal performance. Small details matter. Diffusion depth, oxygen control, and sintering temperature can change results significantly.
The picture is not flawless. Supply concentration creates price and continuity risks, especially when export policies or mining disruptions affect dysprosium availability. The IEA also warns that geographic concentration makes critical-mineral supply chains vulnerable. Manufacturers therefore need traceable inputs, batch testing, and clear magnetic specifications. Some performance claims still deserve closer examination. A low dysprosium percentage does not automatically mean better efficiency. Independent testing remains necessary for coercivity, remanence, temperature stability, and corrosion resistance.
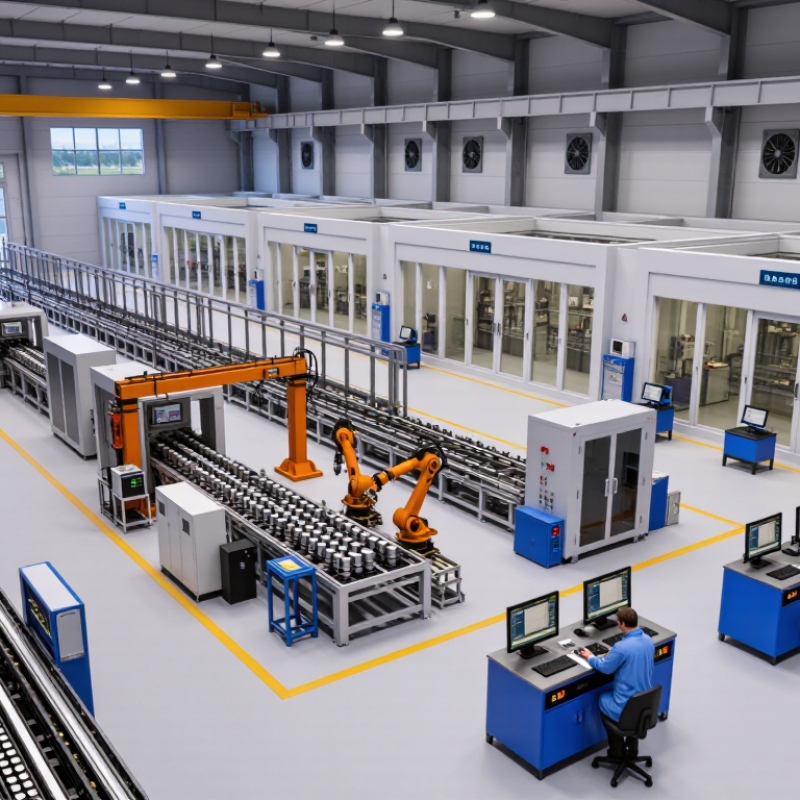
Dy-doped neodymium magnet production requires controlled chemistry and disciplined process management. Manufacturers begin by testing neodymium, iron, boron, and dysprosium raw materials for purity. Alloy melting and strip casting create a uniform starting structure. Hydrogen decrepitation then breaks the alloy into a fragile powder. Jet milling produces fine particles, but particle size must stay consistent. Small variations can affect alignment and magnetic performance.
During pressing, magnetic fields orient the powder before sintering. Vacuum sintering and aging establish density, coercivity, and dimensional stability. Grain boundary diffusion may place dysprosium near grain boundaries, reducing unnecessary heavy-element use. Quality teams inspect magnetic curves, density, dimensions, surface condition, and coating adhesion. They should also verify corrosion resistance through suitable humidity or salt-spray testing. Batch records and traceability support reliable investigations. No process is flawless. A magnet can meet one specification while failing a customer’s actual assembly need.
Tips: Request a complete material report and batch number. Confirm testing methods, not only test results. Check temperature ratings under real operating conditions. Review tolerances for coating thickness, magnetization direction, and size. Independent laboratory verification is valuable for critical applications. Standards such as ISO 9001 can support process consistency, but certification alone does not prove every magnet is suitable. Clear drawings, sample approval, and realistic inspection plans prevent expensive misunderstandings.
| Production Stage | Typical Process Parameters | Primary Quality-Control Dimension | Inspection Method or Reference | Typical Control Target | Common Risk and Preventive Action |
|---|---|---|---|---|---|
| Raw Material Selection | High-purity neodymium, iron, boron and dysprosium-containing feedstock; alloy chemistry is selected according to the required coercivity, temperature capability and magnetic grade. | Elemental composition, trace impurities and batch traceability. | Inductively coupled plasma optical emission spectrometry (ICP-OES), X-ray fluorescence screening and controlled batch records. | Composition must remain within the approved alloy specification; impurity limits are defined by the product design and customer drawing. | Excess oxygen, carbon or metallic impurities can reduce magnetic performance. Use sealed storage, verified certificates and incoming-lot identification. |
| Alloy Melting and Strip Casting | Vacuum or inert-gas melting followed by rapid strip casting to produce a fine, compositionally uniform alloy structure. | Alloy homogeneity, strip thickness, surface condition and absence of visible inclusions. | Metallographic examination, chemical mapping, dimensional checks and visual inspection under controlled lighting. | Uniform strip structure with no significant segregation, cracks, foreign inclusions or abnormal oxidation. | Segregation or oxidation may cause local weak magnetic areas. Control atmosphere, melt temperature, cooling rate and equipment cleanliness. |
| Hydrogen Decrepitation | Hydrogen absorption is used to embrittle the alloy, followed by dehydrogenation or controlled handling before fine milling. | Particle friability, hydrogen removal and powder contamination. | Process pressure and temperature records, residual-hydrogen verification where required, and powder screening. | Powder should be sufficiently friable for milling without uncontrolled oxidation or abnormal agglomeration. | Residual hydrogen and air exposure can affect powder stability. Use controlled transfer and minimize exposure to moisture and oxygen. |
| Jet Milling and Powder Classification | Inert-gas jet milling produces fine NdFeB powder suitable for magnetic alignment and pressing. | Particle-size distribution, oxygen content, flowability and contamination. | Laser diffraction or equivalent particle-size analysis, oxygen/nitrogen analysis and sieve or flow testing. | Many commercial processes target a fine powder distribution commonly centered around approximately 3–8 µm; the approved specification controls the actual range. | Oversized particles may reduce coercivity and alignment quality, while excessive fines can increase oxidation and handling risk. |
| Magnetic Alignment and Compaction | Powder is aligned in a magnetic field and compacted by die pressing or isostatic pressing, depending on geometry and performance requirements. | Easy-axis orientation, green density, dimensional stability and crack control. | Magnetic-field verification, green-body density measurement, dimensional inspection and visual examination. | Typical alignment fields are commonly in the approximate range of 1.5–2.5 T, subject to equipment and formulation; green bodies must be free from visible cracks. | Misalignment lowers remanence. Maintain field uniformity, powder filling consistency, pressing pressure and tooling condition. |
| Vacuum Sintering | Compacted bodies are sintered in a controlled vacuum or inert atmosphere, followed by cooling and, where applicable, aging treatments. | Density, shrinkage, grain structure, dimensional change and magnetic performance. | Temperature-pressure-time records, density measurement, metallography, dimensional inspection and magnetic testing. | Typical final density for sintered NdFeB is approximately 7.3–7.6 g/cm³; the approved grade specification governs acceptance. | Insufficient sintering causes low density; overheating causes grain growth and reduced coercivity. Use calibrated furnace recipes and uniform loading. |
| Dysprosium Introduction | Dy may be incorporated into the alloy or introduced locally by grain-boundary diffusion to improve coercivity and high-temperature resistance. | Dy distribution, diffusion depth, coercivity improvement and retention of remanence. | Cross-sectional SEM/EDS mapping, chemical analysis, magnetic-property testing and process-record review. | Diffusion depth and Dy concentration profile must match the approved technical specification; excessive Dy can reduce remanence and increase material cost. | Nonuniform diffusion creates local magnetic variation. Control coating or source loading, diffusion temperature, holding time and surface cleanliness. |
| Machining and Sizing | Diamond grinding, slicing, drilling or other non-ferrous machining is used to achieve drawing dimensions. | Length, width, thickness, parallelism, perpendicularity, chamfer and surface damage. | Calibrated micrometers, gauges, optical measurement systems, surface inspection and sampling plans. | Dimensional tolerances are controlled according to the customer drawing; general tolerances may be referenced to ISO 2768 where applicable. | NdFeB is hard and brittle. Use suitable coolant, controlled feed rates, edge protection and separation of magnetic parts during handling. |
| Surface Treatment | Common protective systems include nickel-based multilayers, epoxy, zinc or other specified coatings selected for the service environment. | Coating thickness, adhesion, coverage, appearance and corrosion resistance. | Magnetic or eddy-current thickness measurement, cross-cut or pull-off adhesion testing, visual inspection and humidity or salt-spray testing where specified. | Coating type and thickness must follow the drawing or purchase specification; test duration and acceptance criteria should be agreed before production. | Pinholes and poor adhesion accelerate corrosion. Control pre-cleaning, activation, bath chemistry, rinsing and drying conditions. |
| Magnetization | Finished parts are magnetized using a pulsed magnetic field with the required pole orientation and magnetization direction. | Magnetization completeness, polarity, field direction and surface flux consistency. | Gaussmeter, Helmholtz-coil measurement, polarity tester and reference fixture. | Polarity and magnetic output must meet the drawing or grade specification; measurements require a defined fixture, temperature and distance. | Incorrect orientation or insufficient pulse energy causes rejects. Use keyed fixtures, verified pulse settings and polarity checks. |
| Magnetic Property Testing | Magnetic performance is evaluated after stabilization and conditioning at the specified measurement temperature. | Remanence (Br), intrinsic coercivity (Hcj), coercive force (Hcb) and maximum energy product ((BH)max). | Hysteresisgraph or permeameter testing; ASTM A977/A977M may be used as a reference for permanent-magnet material measurements. | Values must meet the approved material grade and product specification; Dy-containing grades are generally selected when higher Hcj or temperature capability is required. | Fixture errors, incorrect sample orientation and temperature variation affect results. Calibrate instruments and retain measurement records. |
| Temperature and Environmental Verification | Parts may be evaluated under elevated-temperature exposure, thermal cycling, humidity or corrosion conditions according to the application. | Irreversible flux loss, dimensional stability, coating durability and corrosion resistance. | Thermal chamber testing, pre- and post-test magnetic measurement, humidity testing and salt-spray testing when specified. | Acceptance limits are application-specific and should include test temperature, exposure time, fixture condition and allowable magnetic loss. | High temperature can cause irreversible demagnetization; select adequate Hcj, coating and thermal design margins. |
| Final Inspection and Sampling | Final inspection combines dimensional, visual, magnetic, coating, packaging and traceability checks before release. | Conformity to drawing, lot identity, quantity, appearance and test documentation. | 100% checks for critical characteristics where required; statistical sampling may reference ISO 2859-1. | Critical characteristics require zero-defect or tightened acceptance criteria when defined by the customer; sampling levels must be documented. | Mixed lots and incomplete records create traceability risk. Use barcode or batch identification and retain inspection reports. |
| Compliance and Packaging | Magnets are packed with separators and protective materials suitable for shipment, storage and magnetic-field restrictions. | Packaging integrity, corrosion protection, labeling, transport safety and restricted-substance compliance. | Packaging inspection, label verification, documentation review and applicable RoHS or REACH declarations. | Packaging and declarations must match destination-market requirements and the customer’s logistics specification. | Impact, moisture and uncontrolled magnetic fields can damage products or create transport issues. Use dry packaging, cushioning and appropriate magnetic shielding. |
Technical note: The parameter ranges shown are representative industry ranges rather than universal acceptance limits. Final limits should be established in the approved material specification, engineering drawing, control plan and customer order. Dy-containing NdFeB magnets may be produced by bulk alloying, grain-boundary diffusion, or a combination of both methods.
China Top Dy Doped Neodymium Magnets Manufacturers
Evaluating leading Chinese magnet manufacturers requires more than comparing prices. The IEA’s Global Critical Minerals Outlook 2024 reported that China produced about 94% of the world’s sintered permanent magnets. This scale creates strong manufacturing depth, but it does not guarantee consistent Dy-doped NdFeB quality. Ask for batch-level data, including remanence, intrinsic coercivity, maximum energy product, and temperature coefficients. Request test methods and equipment details, not only a polished certificate.
Check how dysprosium is introduced. Grain-boundary diffusion can reduce heavy rare-earth use while improving high-temperature coercivity, but coating thickness and diffusion control matter. A reliable supplier should provide composition records, sintering parameters, magnetic test curves, and traceability from raw material to finished block. The USGS Mineral Commodity Summaries 2024 estimated China’s rare-earth mine production at 240,000 metric tons of rare-earth-oxide equivalent in 2023. That supply advantage may support competitive pricing, yet material origin alone says little about process discipline.
Visit the factory when possible. Observe furnace maintenance, calibration labels, humidity control, and sampling practice. ISO 9001 certification helps, but it is only a starting point. I would also compare third-party inspection results with internal reports and test samples after thermal aging. Small differences can become motor failures. No checklist is perfect. Procurement teams sometimes overvalue certificates and undervalue field feedback, which is a costly weakness. Ask for corrective-action records, realistic lead times, packaging specifications, and evidence from comparable applications.
Dy-doped neodymium magnets support high-temperature applications where ordinary neodymium magnets may lose performance. Common uses include electric vehicle motors, industrial robots, wind generators, pumps, and compact sensors. Dysprosium can improve coercivity, especially near heat-producing motor components. However, excessive dysprosium may reduce magnetic strength and increase cost. The design must balance both factors.
Reliable manufacturers usually control alloy composition, grain structure, sintering, machining, and surface protection. Ask for magnetic grades, temperature coefficients, dimensional tolerances, and test reports. A practical factory audit should review batch records, calibration systems, and coating thickness. Small defects matter. A chipped corner can affect assembly clearance or corrosion resistance.
Supply chains depend on neodymium, praseodymium, dysprosium, iron, and boron. Availability and pricing can change with mining policies, refining capacity, energy costs, and transport conditions. Buyers should request origin information and batch traceability. Dual sourcing may reduce disruption, but it can create slight performance differences. That risk needs testing.
Purchasing teams should define magnet shape, magnetization direction, operating temperature, coating, packaging, and annual volume before requesting quotations. For automotive or other demanding equipment, samples should undergo thermal aging, pull-force checks, dimensional inspection, and corrosion testing. A low unit price can hide higher rejection costs. Forecasts are rarely perfect. Keep realistic safety stock, but avoid storing magnets without moisture control and protective packaging.